Lab-to-Bulk Bioscouring Scale-Up for Cotton Knit Dyehouses
In cotton knit dyeing, bioscouring is only valuable when it scales cleanly from a beaker result to a stable jet-dyeing recipe. The lab may show fast wet-out and good absorbency, but bulk production has different liquor movement, rope packing, fabric tension, temperature ramp behavior, and lot-to-lot cotton variability.
For a dyehouse technical manager searching for an enzyme supplier for cotton bioscouring, the buying question is not simply whether the enzyme works. The question is whether the supplier can help you move from trial fabric to repeatable bulk lots without compromising shade consistency, hand feel, dye uptake, or machine productivity.
What changes when bioscouring leaves the lab
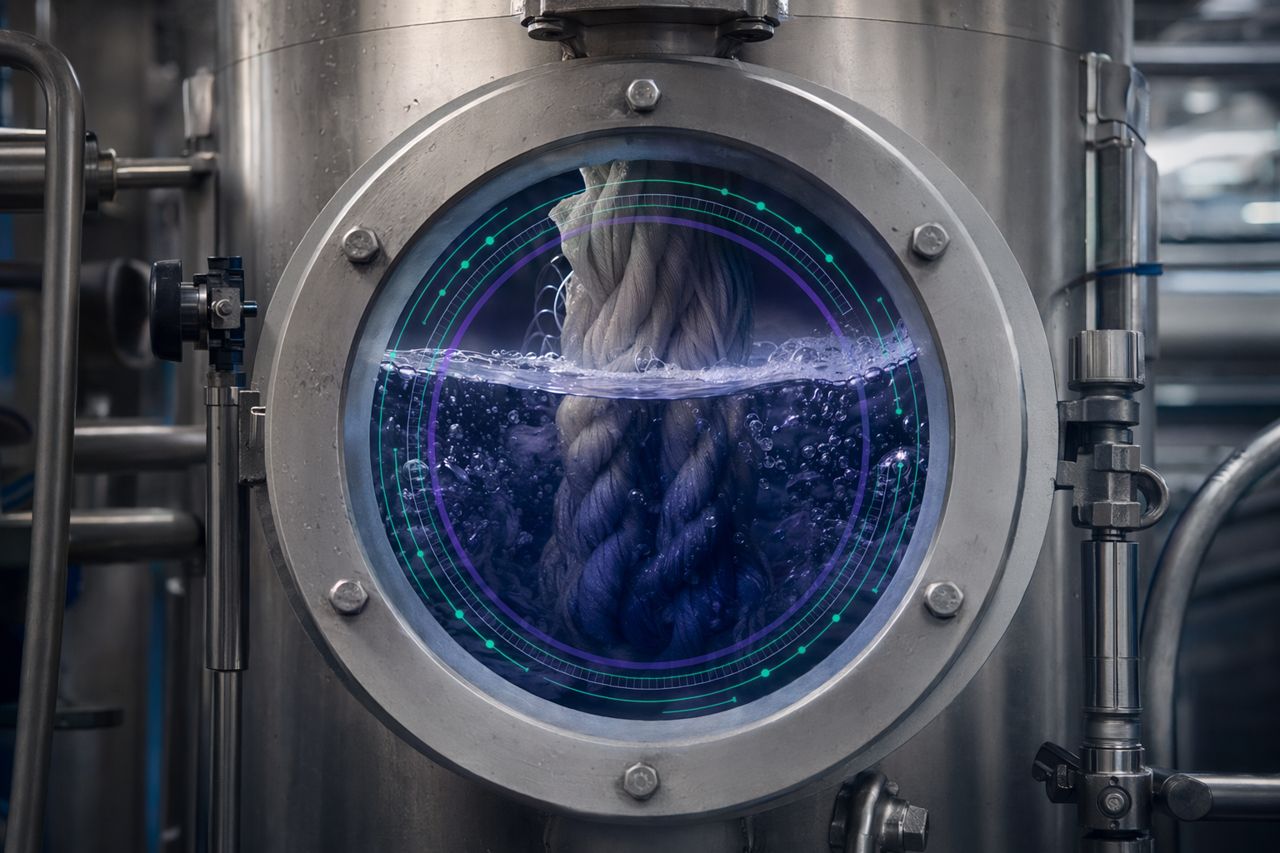
Lab trials usually make fabric access easy. Bulk jets do not. A cotton knit rope can hide waxy zones, trapped air, uneven liquor exchange, and local differences in mechanical action. These differences affect absorbency and can show up later as unlevel dyeing, inconsistent shade depth, or longer corrective work.
Key scale-up differences include:
- Liquor circulation: bulk flow must reach the full rope, not only the visible surface.
- Fabric loading: tighter loading can slow wet-out and reduce contact uniformity.
- Temperature profile: heating behavior in production can differ from lab equipment.
- pH control: drift during processing can reduce process confidence.
- Auxiliary compatibility: wetting agents, sequestrants, buffers, and residual chemistry can change bioscouring performance.
- Cotton variability: wax, pectin, seed coat fragments, and storage history vary between lots.
A good scale-up plan treats bioscouring as part of the complete pretreatment and dyeing route, not as a single isolated enzyme addition.
Start with the commercial target, not the lab result
Before running trials, define what the plant needs the bioscouring step to deliver. The target should be practical, measurable, and connected to production decisions.
Useful scale-up targets include:
- Consistent fabric wet-out before dyeing.
- Improved absorbency across the rope, not just from edge samples.
- Stable shade build in the first-pass dyeing recipe.
- Reduced need for corrective reprocessing caused by uneven preparation.
- Compatibility with current jet machines and standard operating windows.
- Maintained knit hand feel and fabric appearance.
- Cleaner transition into reactive dyeing or combined preparation routes where applicable.
The lab result should be judged against these plant targets. A beautiful beaker trial is not enough if it requires impractical hold times, narrow handling conditions, or recipe changes that disturb the dyehouse schedule.
Build the lab trial around the bulk machine reality
The lab should model production constraints as closely as possible. That does not mean copying every machine detail. It means testing the factors most likely to affect bulk performance.
Include the actual fabric risk profile
Use representative greige cotton knit lots, including fabrics that commonly create problems:
- Compact single jersey.
- Rib and interlock constructions.
- Elastane blends where allowed by the route.
- Higher wax lots.
- Stored or variable-origin cotton lots.
- Dark-shade programs where preparation variation becomes visible.
Test recipe compatibility early
Bioscouring rarely runs alone. Review compatibility with the intended dyehouse route:
- Wetting and penetrating agents.
- Sequestrants and water hardness management.
- pH adjustment system.
- Peroxide or caustic residues if the route includes other preparation steps.
- Silicone, softener, or finishing residues on rework fabric.
- Dye class and shade family used after preparation.
This is where supplier support matters. An enzyme supplier for cotton bioscouring should help identify chemistry conflicts before they appear as shade variation in production.
Move from lab to pilot with controlled questions
A strong scale-up does not try to answer everything in one bulk lot. It uses staged questions.
Stage 1: lab confirmation
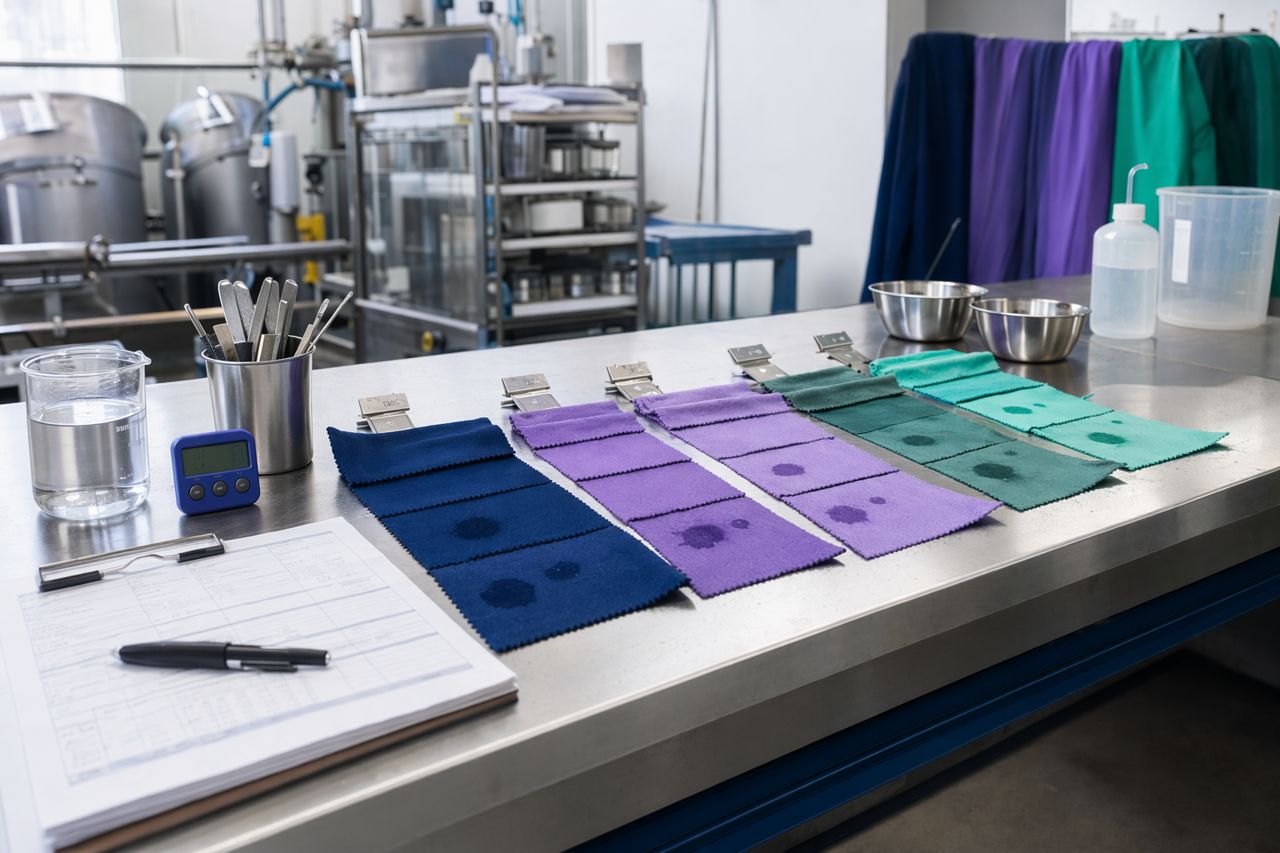
Confirm that the selected bioscouring recipe improves wetting and absorbency on representative fabric. Compare against the current pretreatment route and record fabric handle, appearance, and dyeability indicators.
Stage 2: machine-relevant pilot
Run a small production-like trial where liquor movement, loading, and heating profile better resemble the real jet process. Check whether the fabric rope wets evenly and whether sampling from multiple positions gives a consistent result.
Stage 3: first controlled bulk
Use a defined bulk lot with clear acceptance criteria. Keep the downstream dyeing recipe as stable as possible so that preparation performance is easier to read.
Stage 4: repeat lot confirmation
Repeat on a different fabric lot or shade program. One successful bulk is useful. Repeatability is what creates operating confidence.
What to measure during scale-up
Avoid relying on one pass/fail result. Bioscouring performance should be read through a set of practical dyehouse indicators.
Preparation indicators
- Drop absorbency behavior across several fabric positions.
- Wet-out uniformity in the rope.
- Visual cleanliness and absence of oily or waxy patches.
- Fabric hand and surface appearance.
- Consistency between center, edge, and rope-position samples.
Dyeing indicators
- First-pass shade match behavior.
- Levelness after standard dyeing.
- Shade depth compared with the existing preparation route.
- Rinse behavior and clarity of process transition.
- Need for additional correction, stripping, or reprocessing.
Production indicators
- Ease of operator control.
- Fit with current batch timing.
- Compatibility with existing equipment.
- Chemical handling simplicity.
- Reduced risk of preparation-related downtime.
The objective is not only better absorbency. The objective is controlled preparation that protects bulk dyeing performance.
Common scale-up failure points
Bioscouring problems in bulk are often caused by process fit, not by the enzyme alone.
Uneven liquor access
If the cotton knit rope is packed too tightly or circulation is weak, enzyme contact becomes uneven. The result can be mixed absorbency and visible dyeing variation.
pH drift
A recipe may begin in the correct range but move during processing because of residual alkalinity, incoming water, or fabric carryover. pH control should be checked in the real process, not assumed from lab work.
Auxiliary interference
Some wetting systems, residual oxidants, high alkalinity, or incompatible additives can reduce the practical effect of bioscouring. Compatibility checks should be part of supplier qualification.
Overcorrecting the recipe
Increasing additions to compensate for weak bulk performance may hide the real cause. Before changing the recipe, check loading, circulation, temperature profile, pH stability, and fabric variability.
Testing only easy fabric
A bioscouring route that works only on low-risk fabric may not protect commercial production. Include the constructions and cotton sources that create real dyehouse pressure.
A practical bulk trial checklist
Use this checklist before approving a bioscouring recipe for routine cotton knit production.
Before the trial
- Confirm fabric construction, lot history, and greige condition.
- Define the current benchmark pretreatment route.
- Agree target absorbency and dyeing acceptance criteria.
- Lock the downstream dyeing recipe for comparison.
- Confirm pH and temperature control approach.
- Review auxiliary compatibility.
- Identify sampling points from multiple rope positions.
During the trial
- Record loading, liquor movement, process timing, and temperature profile.
- Monitor pH at defined points.
- Observe wet-out and rope behavior.
- Keep operator notes on foam, handling, and flow.
- Avoid unplanned recipe changes unless needed for safety or quality protection.
After the trial
- Test absorbency from multiple locations.
- Dye using the agreed comparison route.
- Review levelness, shade depth, and first-pass match.
- Compare hand feel and visual cleanliness.
- Record whether any corrective work was needed.
- Decide whether the next step is repeat trial, recipe adjustment, or production approval.
How supplier support should look
The right enzyme partner should support the dyehouse with practical process guidance, not just product literature.
For cotton knit bioscouring, useful supplier support includes:
- Recipe screening against your existing pretreatment and dyeing route.
- Guidance on operating windows that fit jet-dyeing practice.
- Compatibility review with auxiliaries already used in the plant.
- Trial planning for lab, pilot, and controlled bulk runs.
- Troubleshooting for uneven wet-out, shade variation, and pH drift.
- Documentation that helps operators run the process consistently.
- Commercial supply planning for repeat production.
This is the difference between buying an enzyme and qualifying an enzyme process.
Commercial value for the dyehouse
A well-scaled bioscouring route can help the dyehouse reduce uncertainty before the dye bath. The value is seen in better preparation control, fewer surprises during dyeing, and a more dependable route for cotton knit programs.
Potential plant-floor advantages include:
- More uniform wetting before dyeing.
- Improved confidence in shade consistency.
- Lower risk of rework linked to poor preparation.
- Gentler preparation conditions where the full route allows.
- Better alignment between lab approval and bulk production.
- Clearer troubleshooting when fabric, water, or machine conditions change.
The commercial win is not a single trial result. It is a repeatable preparation step that protects schedule, shade, and customer commitments.
When to request a quote
Request a quote when you can share the fabric type, current pretreatment route, target dyeing program, machine type, and the problem you want to solve. That information allows LoopBath to recommend a bioscouring approach that fits the plant rather than forcing a generic recipe into production.
Request a quote for cotton knit bioscouring support
Quick information to include in the quote form
To speed up technical review, include:
- Cotton knit construction and typical batch size.
- Current scouring or preparation route.
- Dyeing machine type and process constraints.
- Main quality issue: absorbency, shade levelness, rework, hand feel, or process simplification.
- Key auxiliaries used in pretreatment.
- Target shade families and downstream dyeing route.
- Whether you need lab screening, pilot support, or bulk conversion guidance.
LoopBath can then respond with a focused recommendation for cotton bioscouring scale-up in your dyehouse context.